Every fixture below represents a fully customizable engineering baseline. Available with global voltage driver integration (120V-277V), certified wet/damp ratings, custom color temperatures, and bespoke material finishes.
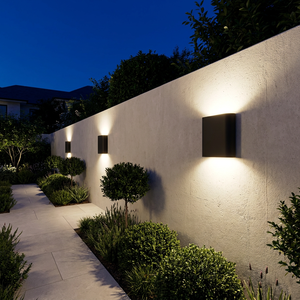
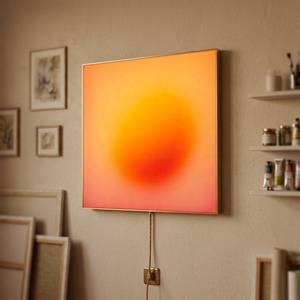
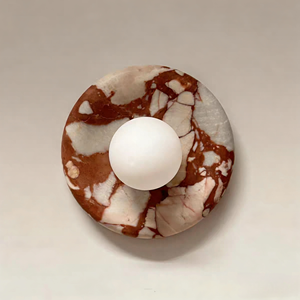
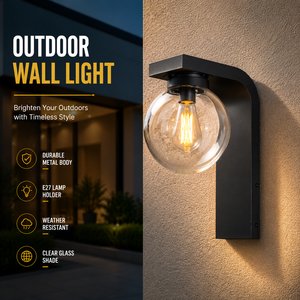
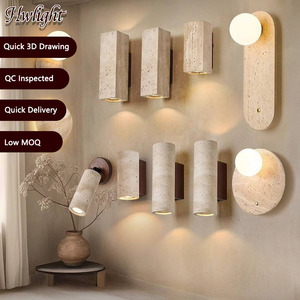
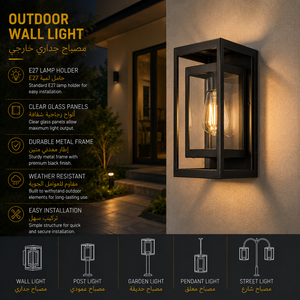
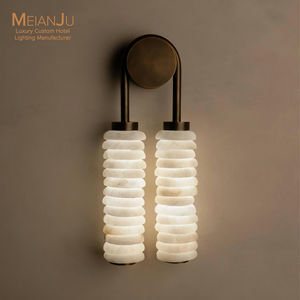
In modern architectural procurement, the gap between conceptual lighting design and commercial implementation presents continuous challenges in weight distribution, thermal efficiency, and global regulatory compliance. As a premier Custom OEM Project Lighting Exporter, our manufacturing model integrates design validation, precision metalwork, artisan stone processing, and photometrical certification under a unified quality assurance protocol.
Every custom inquiry is converted into detailed 2D/3D shop drawings. We analyze structural loads, mounting canopy geometry, driver enclosure ventilation, and voltage requirements prior to raw material cutting, preventing costly field modifications.
From heavy-gauge ADC12 die-cast aluminum for wet-rated exterior sconces to hand-forged solid copper and wrought iron chassis, our metallurgy workshops maintain ultra-strict tolerances (±0.2mm) to ensure seamless architectural integration.
We work directly with raw Spanish alabaster blocks, Italian travertine, and hand-blown studio glass. CNC carving combined with manual hand-finishing allows custom translucent diffusion while retaining natural mineral veining uniqueness.
Comparison of material behaviors, ingress protection ratings, and optical options for project-level customization.
| Material / Component | Primary OEM Application | Thermal / Environmental Rating | Customization Scope |
|---|---|---|---|
| Die-Cast ADC12 Aluminum | Exterior Villa Wall Sconces, Commercial Facades | IP65 / IP67 Wet Location, -40°C to +50°C | Custom powder coating, anti-saline marine finishes, 5CCT optics switch. |
| Natural Spanish Alabaster | Luxury Hotel Corridors, High-End Foyer Sconces | Indoor / Damp Location, Low thermal expansion | Vein density selection, block carving thickness (10mm-25mm), custom seals. |
| Porous Wabi-Sabi Travertine | Bespoke Interior Sconces, Villa Ambient Lighting | Dry / Indoor Damp, Natural acoustic absorption | Surface filler option, edge chamfering, concealed backlighting LED channel. |
| Optical Grade Acrylic (Gradient) | Backlit Art Sconces, Commercial Mood Boxes | UV-Stabilized, Anti-yellowing (10-Year Guarantee) | Silk-screen pattern embedding, gradient tinting, RGBW / Tunable White engine. |
| Solid Copper & Brass Alloys | Heritage Restorations, Luxury Resort Luminaires | Corrosion-resistant, Patina self-healing layer | Hand-rubbed oil bronze, polished brass, antique oxidation, protective clear-coat. |
The global project lighting market is undergoing a structural transformation. Commercial specifiers, hospitality developers, and international procurement agencies no longer evaluate luminaires purely by aesthetic criteria. Today’s decision-making matrix is anchored in modular serviceability, field-configurable optics, multi-voltage driver standardization, and material circularity.
Stock management risks across global hospitality developments have driven demand for 5CCT selectable drivers (2700K/3000K/3500K/4000K/5000K) and wattage-tunable dip switches. OEM customization now demands integrated CCT toggles behind IP65 sealed gaskets, enabling on-site lighting tone adjustment during project commissioning.
Modern architectural design trends—specifically Wabi-Sabi, Biophilic, and Nordic Minimalist styles—have elevated raw materials like Italian Travertine and Spanish Alabaster. As an experienced exporter, our OEM manufacturing process bridges raw stone cutting with precision thermal heat sinks, protecting delicate stone from LED driver thermal stress.
Large-scale OEM installations require seamless interoperability with legacy and modern building management systems (BMS). Our custom driver cavities are engineered to house DALI-2, 0-10V, Phase-Cut, Zigbee, and Casambi wireless nodes, enabling individualized room control or full building automation without altering the aesthetic profile of the fixture.
For seaside resort projects, standard powder coating fails prematurely due to salt-spray oxidation. Advanced OEM manufacturing incorporates multi-stage chromate conversion pretreatment followed by architectural fluorocarbon (PVDF) electrostatic spraying, reaching 2,000+ hours in salt-spray chamber testing.
Unlike trading intermediaries that outsource production across fragmented job shops, our centralized manufacturing infrastructure handles raw material cutting, metal forging, CNC milling, surface finishing, wiring assembly, photometric integration, and UL drop-test packaging under one roof. This single-source accountability guarantees consistent lot-to-lot color matching, verified lead times, and comprehensive warranty coverage.
In-depth technical answers addressing engineering verification, international certification, lead-time logistics, and custom OEM project workflows.
Yes. Our in-house engineering design team specializes in converting concept sketches, architectural renderings, or 2D/3D CAD models into fully realized production shop drawings. We generate comprehensive engineering submittal packages that detail structural mounting points, overall weight, electrical load, LED driver thermal dissipation paths, and exact material specifications. Fabrication begins only after formal written shop drawing approval from your design team.
All OEM fixtures are engineered and tested to satisfy UL 1598, cUL, CE, and RoHS safety standards. For global export programs, we integrate universal voltage drivers (120-277V, 50/60Hz) or region-specific drivers (220-240V for Europe/Middle East/Asia). Fixtures designated for outdoor, resort, or wet locations undergo IP65/IP66 pressurized water spray testing, complete with high-temp silicone seals and pressure-equalization strain relief glands.
Standard prototyping and shop drawing verification typically require 10 to 15 business days. Once prototypes and shop drawings receive final sign-off, full project production runs generally ship within 4 to 6 weeks, depending on material complexity (e.g., custom alabaster carving vs. standard die-cast aluminum). Because all forging, CNC machining, glass crafting, and finishing are performed within our facility, we control timelines internally without third-party delay risks.
We provide complete IES photometrics, spectral distribution charts, CRI/R9 values, thermal testing reports, and step-by-step installation guides for architectural specifiers and lighting designers. Photometric data can be imported directly into DIALux or Relux lighting calculation software to verify lux levels and glare control (UGR) for commercial space compliance.
Export packaging utilizes multi-layer high-density molded polyethylene (EPE) foam cut via CNC to match the exact profile of each component. Delicate stone diffusers and blown glass elements are individually isolated within heavy-duty 7-ply corrugated export cartons, reinforced with corner guards and packed inside ISPM-15 compliant heat-treated wooden crates for containerized ocean or air freight.
We accommodate both boutique luxury projects and large-scale commercial developments. While mass die-cast production reaches optimal unit economics at 50+ units, our custom hand-crafted and CNC stone/metal operations support small-batch production for specialized boutique hotel runs, high-end private villas, or mockup mock-room installations.
Submit your project elevations, CAD drawings, or custom product specifications directly to our engineering department. Receive shop drawing support, photometric data, and factory-direct pricing within 24 hours.